


SABCA · Performant Industries · Lummen, Belgium
From machine to model
Machine data, vision inspection and models on one platform — anomalies visible during layup instead of at final inspection.
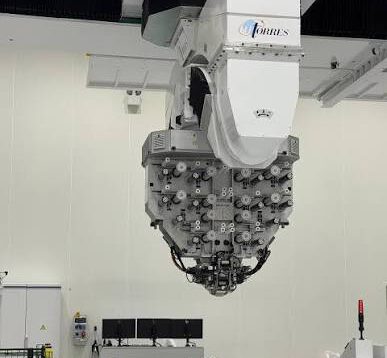
Automated fiber placement builds up an aircraft structure tape by tape over many hours, and a deviation only becomes visible at final inspection, when the part is finished. A small process anomaly turns into scrap, rework and an unpredictable lead time. The data that would explain it sits apart: control on the PLC, sensors on the floor, results in quality systems. Nothing links a measured process to a measured outcome.
Result
- Machine, environment and inspection data joined in one neutral platform.
- Traceable production history per part, reusable for maintenance and reporting.
- Anomalies visible during layup instead of at final quality control.
- Less scrap, less idle time, and a predictable lead time for the end customer.
What we did
Boolean builds the data layer and the models on top of it. We capture machine and environment parameters live from the AFP machine, add automated visual inspection of the layup, and land everything in one vendor-neutral historian with full context: which program, which ply, which conditions. On that layer we train models per question: quality, energy use and machine wear, each validated against real inspection results. Operators see it in a dashboard; nothing leaves the site.
How we delivered it
The project runs in phases: first the neutral data platform and the measurement setup, then vision-based in-process inspection, then the predictive models. Boolean works alongside SABCA Limburg's production and quality teams and research partner Flanders Make. Each phase is usable on its own (the platform already gives traceable production data before the first model goes live), so value does not wait for the end of the project.
In detail
How it works
A digital twin is not a 3D render. It is a measured process, linked to a measured outcome, and a model that learns the relation between the two. This page shows how that is put together on the shop floor.
Technical detail
Capture starts at the machine. Control and process parameters are read from the PLC over Modbus TCP, environmental and auxiliary measurements are published over MQTT, and a vision setup inspects the layup while the head keeps running. Everything lands in one time-series database with context attached (program, ply, tool, conditions), so a measurement can always be traced back to the part it belongs to. The platform is vendor-neutral and runs virtualised on site: production data stays in-house, and inspection results flow back in as training labels.
In daily use
Operators get a live view of the run and a signal when the process drifts outside what the model recognises as good, early enough to correct instead of scrap. Engineers use the same history to see why a part behaved the way it did, and maintenance uses the machine data for planned rather than reactive intervention. Three model families run on one platform: quality prediction, energy and peak use, and machine wear, each validated against real inspection results before production trusts it.
Client

Ready to put your data to work?
We think along from the very first conversation. No standard answer, but a plan tailored to you.